|
|
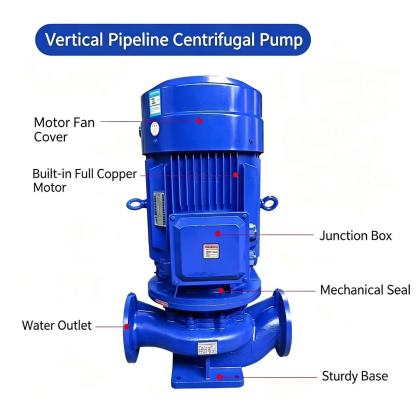
ISG Vertical Pipeline Centrifugal Pump Explosion Proof Motor OptionIndustrial fluid handling environments often contain flammable gases, volatile vapors and combustible fine particles that create potential explosion hazards during equipment operation. For ISG vertical pipeline centrifugal pumps deployed in chemical processing, petrochemical transportation, pharmaceutical production and fuel circulation systems, the explosion proof motor option serves as a critical safety configuration to adapt to hazardous working conditions. This specialized motor configuration eliminates potential ignition sources generated by electrical operation, mechanical friction and temperature rise, allowing vertical pipeline pump units to operate stably and safely in classified explosive atmospheres while maintaining standard fluid conveying performance.
Professional Explosion Proof Grading and Standard ComplianceThe explosion proof motor option for ISG vertical pipeline centrifugal pumps follows international industrial safety standards to achieve hierarchical protection matching for different hazardous environments. Compliance with IEC 60079 and ATEX directives ensures the motor meets unified safety specifications for explosive gas atmospheres used in global industrial sites. Different explosion proof grades correspond to distinct environmental hazard levels, covering Zone 1 continuous hazardous environments and Zone 2 intermittent hazardous environments where flammable mixtures may appear under abnormal operating conditions. Reasonable gas group and temperature class matching further standardizes the safety performance of explosion proof motors. Common classification standards include IIA, IIB and IIC gas groups applicable to different flammable medium volatility, while T3 to T6 temperature classes control the maximum surface operating temperature of the motor. This graded design prevents motor surface overheating from igniting surrounding flammable gases and vapors, achieving targeted explosion suppression for various industrial pipeline medium scenarios. Strict standard compliance ensures the motor eliminates electrical spark leakage and high-temperature ignition risks during long-term continuous pump operation. Structural Design of Explosion Proof Motor Safety MechanismsThe explosion proof motor option adopts exclusive structural optimization to block internal and external explosion transmission paths, differing fundamentally from ordinary general-purpose motors. Sealed explosion proof enclosures isolate internal electrical components such as stators and rotors from external explosive atmospheres. Precision-fit gap structures are designed at assembly joints and shaft penetration positions, which can cool and extinguish sparks and high-temperature gas generated by internal electrical faults before they spread to the external environment. Internal component reinforcement and insulation optimization eliminate potential electrical ignition sources. Enhanced insulation materials resist aging and breakdown under long-term variable load operation, preventing electric arc generation caused by short circuits. Meanwhile, optimized rotor dynamic balance and bearing matching structures reduce mechanical friction and abnormal high-temperature accumulation during high-speed rotation. The integrated anti-static and anti-flashover design further avoids static spark generation caused by long-term equipment operation, forming a multi-dimensional safety protection system for explosive working environments. Scenario Adaptability and Operational Safety AdvantagesThe explosion proof motor option provides targeted scenario adaptation for the vertical installation characteristics and continuous operation mode of ISG pipeline centrifugal pumps. Vertical pump layout features stable operation and long uninterrupted running cycles, which puts forward higher requirements for the continuous safety performance of supporting motors. The explosion proof structure reserves stable safety tolerance for long-term operation, avoiding protection performance degradation caused by component aging and minor operational wear. This motor configuration effectively reduces equipment safety risks in complex industrial environments with volatile, flammable and corrosive media. It adapts to frequent start-stop operation and variable pipeline pressure working conditions, maintaining stable explosion proof performance during load fluctuation. In addition, the optimized heat dissipation structure matches the sealed explosion proof design, solving the heat accumulation problem of fully enclosed motors and preventing thermal failure and safety hazards caused by poor heat dissipation. This reliable operational adaptability makes the explosion proof motor option an essential safety configuration for ISG vertical pumps in high-risk industrial fluid transportation scenarios. |